Cold Saw vs Band Saw: Which for Tube and Profile? A Factory Guide
Cold saw vs band saw is the decision every fabrication shop meets twice: once when the first tube saw wears out, and again when volumes grow enough that cut quality starts to cost money. Both machines cut metal with a toothed blade; the difference is thermal. A cold saw turns a circular blade at low speed under flood coolant, so the blade and the workpiece stay near room temperature; a band saw pulls a continuous blade fast through dry or lightly lubricated cuts, trading heat and edge finish for throughput and low blade cost. This guide compares the two on cut quality, heat, speed, blade economics and tube-specific fit, maps real machine classes from our cold saw range with published specs, and shows where a fiber laser tube cutter replaces both.
It is written from the factory floor rather than a showroom. On the factory side, the saw decision is a downstream one: whatever runs before the bender, the chamfering machine or the weld cell needs short, cool, burr-light cuts — everything else is secondary.
What a Cold Saw Is (and Why Heat Matters)
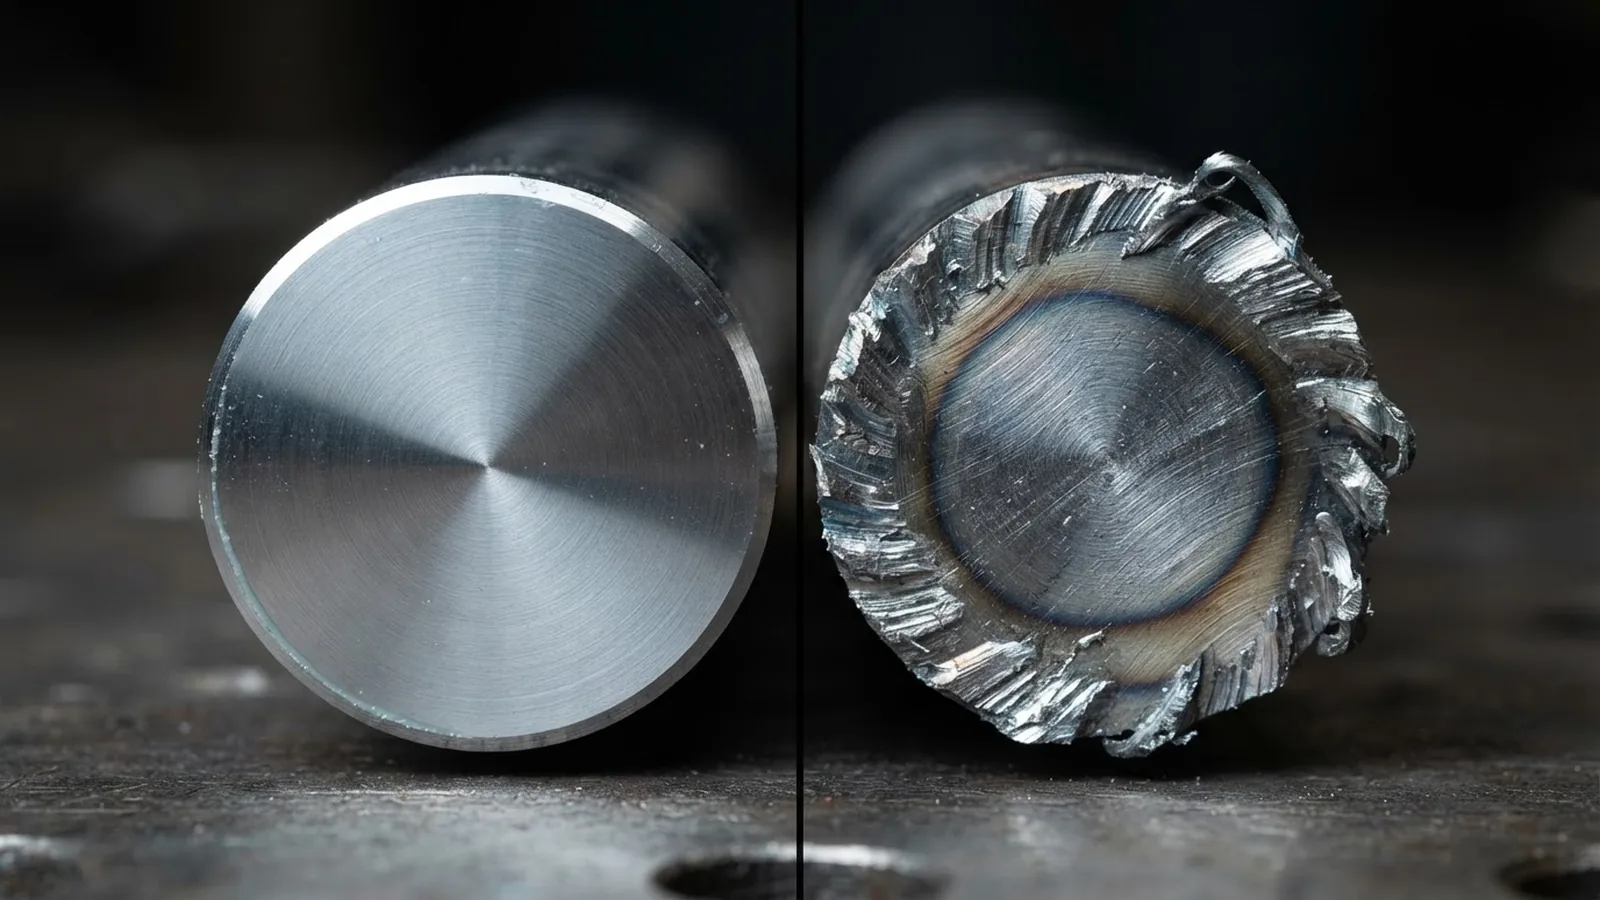
A cold saw drives a large circular blade — HSS or carbide-tipped (TCT) — at surface speeds around 50–100 rpm spindle speed (the published setting on our CTK models), with coolant flooding the cut. The slow speed and the cooling matter for two reasons. First, the blade teeth shear the metal instead of ablating it, so the heat goes into the chip, not the part — the tube comes out touchable and dimensionally stable. Second, a cool cut is a clean cut: minimal burr, no discolored heat-affected zone, and a face that welds or chamfers without extra dressing.
The trade is rate and range: a circular blade only cuts what its diameter can sweep, and each cut takes longer than a fast band blade pulling through the same section.
What a Band Saw Is Built For
A band saw runs a continuous toothed strip at much higher blade speeds, dry or with light lubrication. Heat is the accepted cost: the cut zone runs hot, the finish shows teeth marks and needs deburring, and thin-wall tube can deform under the blade pressure. In exchange you get throughput and reach — band saws slice large solid bar and big beam sections economically, blade replacement is cheap, and the machines tolerate abuse.
For structural steel yards and machine shops cutting solids, that trade is usually right. For tube and profile work feeding downstream processes, the heat and the burr change the math.
Cold Saw vs Band Saw: The Head-to-Head
| Band saw | Cold saw | |
| Cut heat | Hot cut; part can discolor and distort | Cool cut; heat carried away in the chip by coolant |
| Edge finish | Tooth marks, heavy burr, needs dressing | Near-machined face, light burr, weld-ready in many cases |
| Best material shape | Solid bar, beam, large sections | Tube, pipe and profile where finish matters |
| Blade cost | Low per blade | Higher (circular HSS/TCT), but re-sharpenable |
| Repeatability (CNC class) | Good on solids | ±0.1 mm with multi-feed and short tail ends |
| Noise | High whine | Low hum under coolant |
Where Each Fits in a Tube Shop
Mapped against our own cold saw range, the choice by class looks like this — every figure is a published specification from the product page:
| Class | Models | Saw blade | Published capability |
| Руководство | CTK-275B, CTK-300B, CTK-315 | φ250–325 mm | 50–104 rpm two-speed; maintenance and short runs |
| Полуавтоматический | CTK-315AC, CTK-465AC (45°&90°), CTK-450AV, CTK-405AV (φ303–800 mm) | φ250–455 mm (HSS/TCT) | Pneumatic clamping; daily one-piece cutting |
| ЧПУ | CTK-450CNC-3Z, CTK-500CNC, CTK-600CNC | φ250–600 mm (HSS/TCT) | Multi-feed 20–1,900 mm at ±0.1 mm; tail-end 10–100 mm |
Two tube-specific notes from experience. First, the tail-end number is money: on a 6-meter bar of stainless, a CNC cold saw that leaves a 10–20 mm remnant instead of 100 mm keeps sellable stock on every bar — the CNC premium usually pays back there before labor even enters the calculation. Second, miter capability decides machine count: models with 45° heads let one saw feed a frame cell directly instead of a second dedicated miter saw.
Blade Economics: HSS, TCT and Re-sharpening
Blade strategy separates the two systems as much as the machines do. Band saw blades are consumable strips — cheap, replaced, discarded. Cold saw blades are assets: HSS blades for general steel and stainless, TCT for fast, bright finishes on tube, both re-sharpened on a CNC saw blade sharpening machine dozens of times before retirement. A shop running two shifts should budget blades per month and sharpenings per week — and decide the saw partly on the sharpening capacity it will need. We supply both HSS and TCT saw blades as consumables.
When to Skip Both: Fiber Laser Tube Cutting
Saws cut straight lines. The moment the part needs slots, holes, copes or profile-dependent geometry, the saw becomes the first station of a multi-machine chain — and that is where a fiber laser tube cutter absorbs the work: cutting, notching and marking in one clamping, with zero tooling changes between profiles. The honest sequencing we recommend: keep a saw for cheap straight cuts and short runs, and step up to laser when part complexity or batch size makes secondary operations the real cost. The economics of that step are in our tube laser cutting machine price guide.
What to Send for a Quote
- Tube schedule — material, diameter range, wall thickness range, lengths.
- Output — cuts per shift; batch sizes decide manual vs semi-auto vs CNC.
- Downstream process — bending, chamfering or welding after the saw changes the finish requirement.
- Miter needs — 90° only, or 45° compound work.
- Destination and schedule — port and Incoterms, and when the machine must run.
With those five items the export team returns an itemized quote with blade tooling and sharpening capacity included — send your schedule to Chittak.
Часто задаваемые вопросы
Is a cold saw really better than a band saw for tube?
For tube and profile feeding downstream processes — bending, chamfering, welding — yes, usually: the cool, bright, low-burr cut removes a dressing step and protects thin walls. For solid bar and large structural sections, a band saw remains the economical choice.
Can a cold saw cut solid bar, or only tube?
Both — blade diameter sets the section limit, not the shape. A φ450–600 mm cold saw handles solid bar and heavy profiles; the published blade ranges in the table above give the sweep per model.
How long does a cold saw blade last compared to a band blade?
Different lives: a band blade is consumed and replaced; a cold saw blade is re-sharpened many times over a long service life. Cost per cut, not cost per blade, is the comparison that matters — and it favors the cold saw on tube work.
Do I need a CNC cold saw?
If you cut batches to length, yes — multi-feed at ±0.1 mm with a 10–20 mm tail end removes the operator variable and stops throwing away sellable stock. For maintenance cutting and one-off work, a manual or semi-automatic saw is the honest buy.
Get a Factory Quote
Send the tube schedule and the export team will match the saw class, blade tooling and sharpening capacity to your volumes — or show you where a laser replaces the saw altogether. Contact Chittak to start.
ПОПУЛЯРНЫЕ ПУБЛИКАЦИИ
- Cold Saw vs Band Saw: Which for Tube and Profile? A Factory Guide
- Laser Tube Cutting Thickness and Speed: Real Specs from the Factory
- Tube Laser Cutting Machine Price: A Factory Guide to Cost and Quotes
- Как резать трубы из нержавеющей стали с помощью волоконного лазера
- Пример из практики: немецкий производитель мебели сократил время наладки на 73% с помощью CHITTAK
